

 |
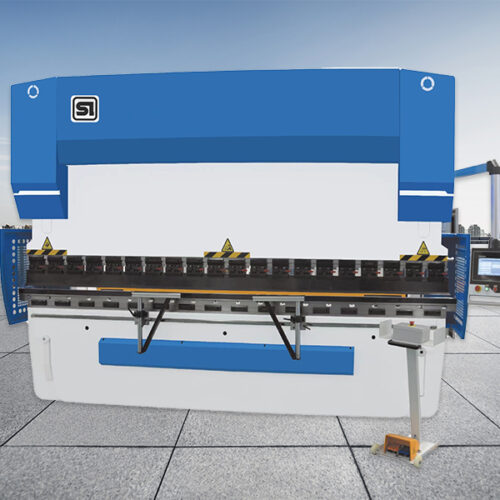
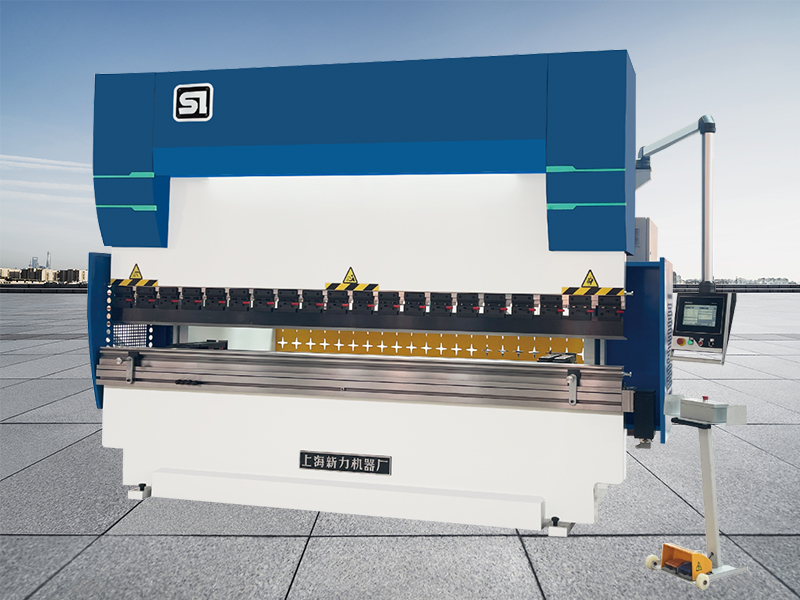
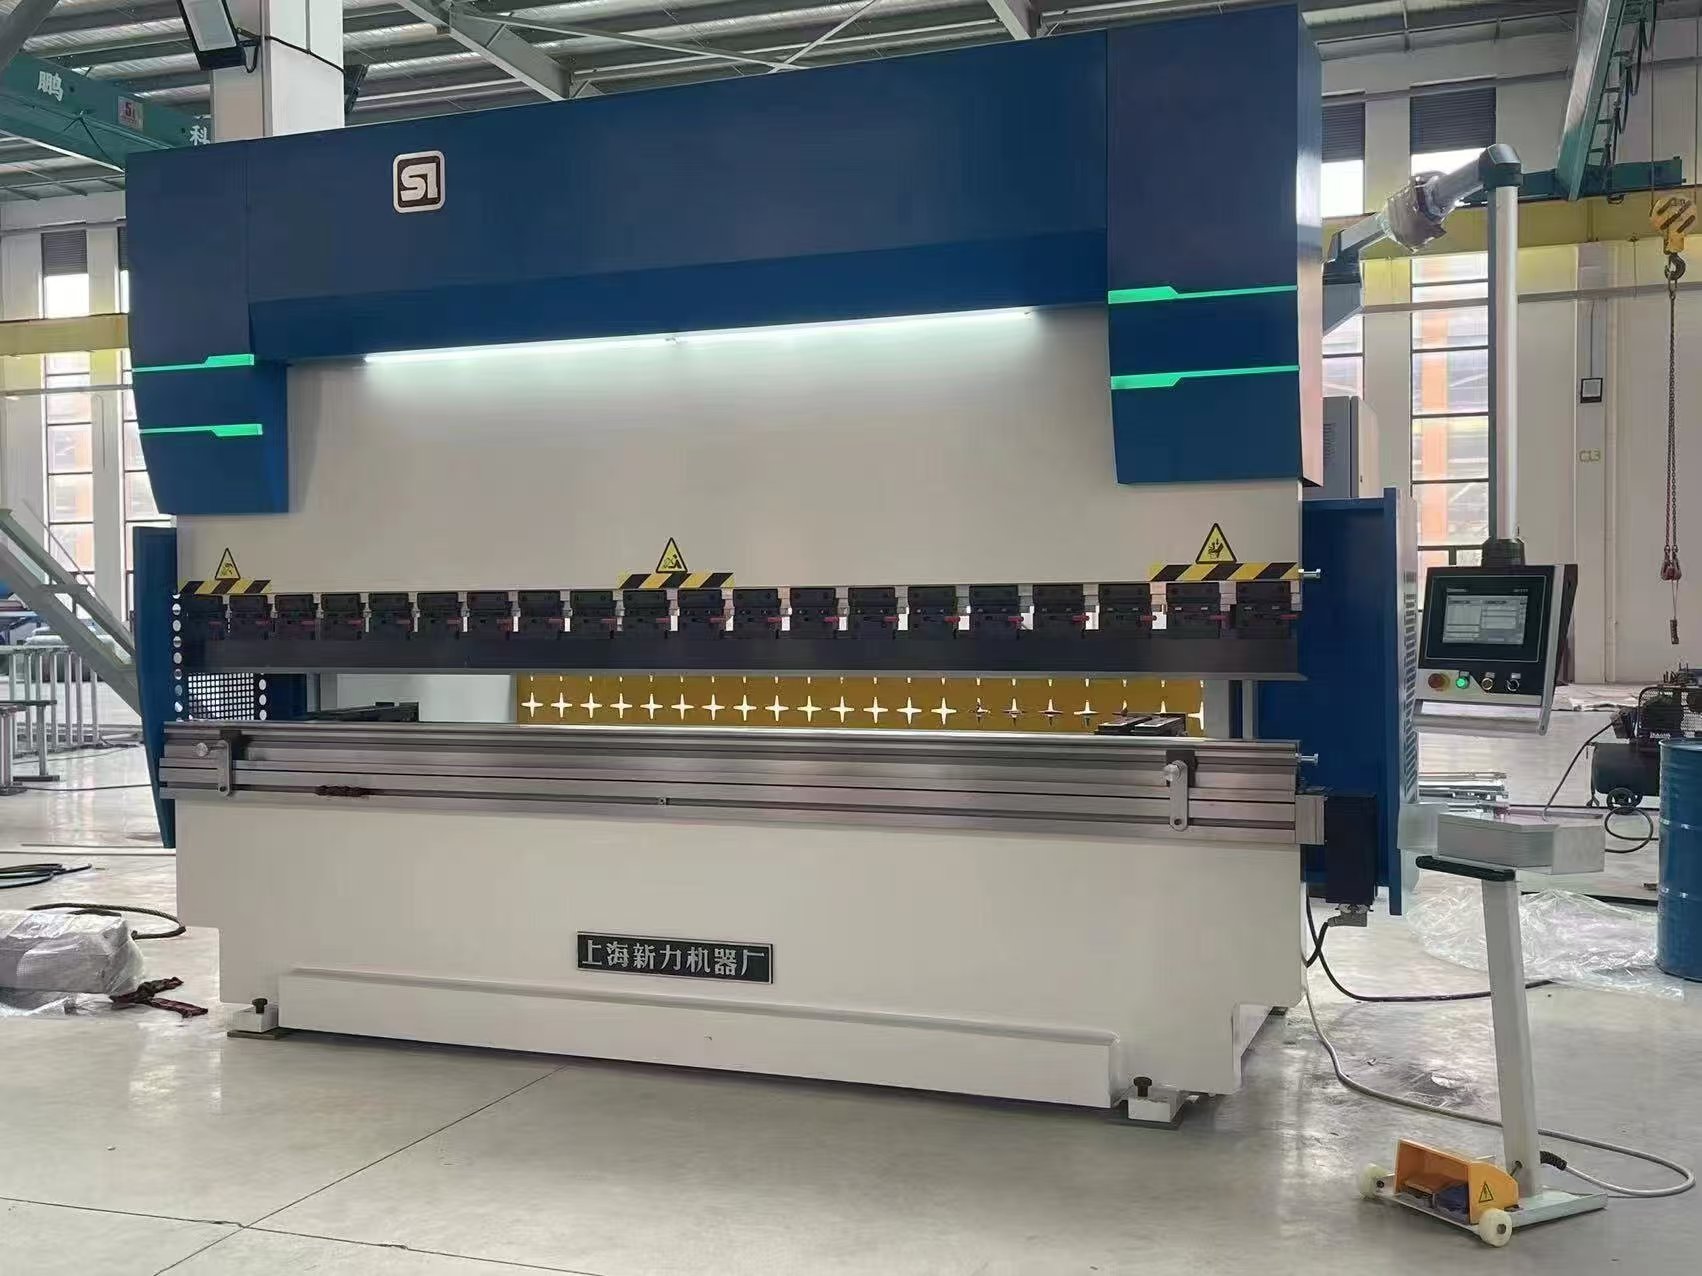
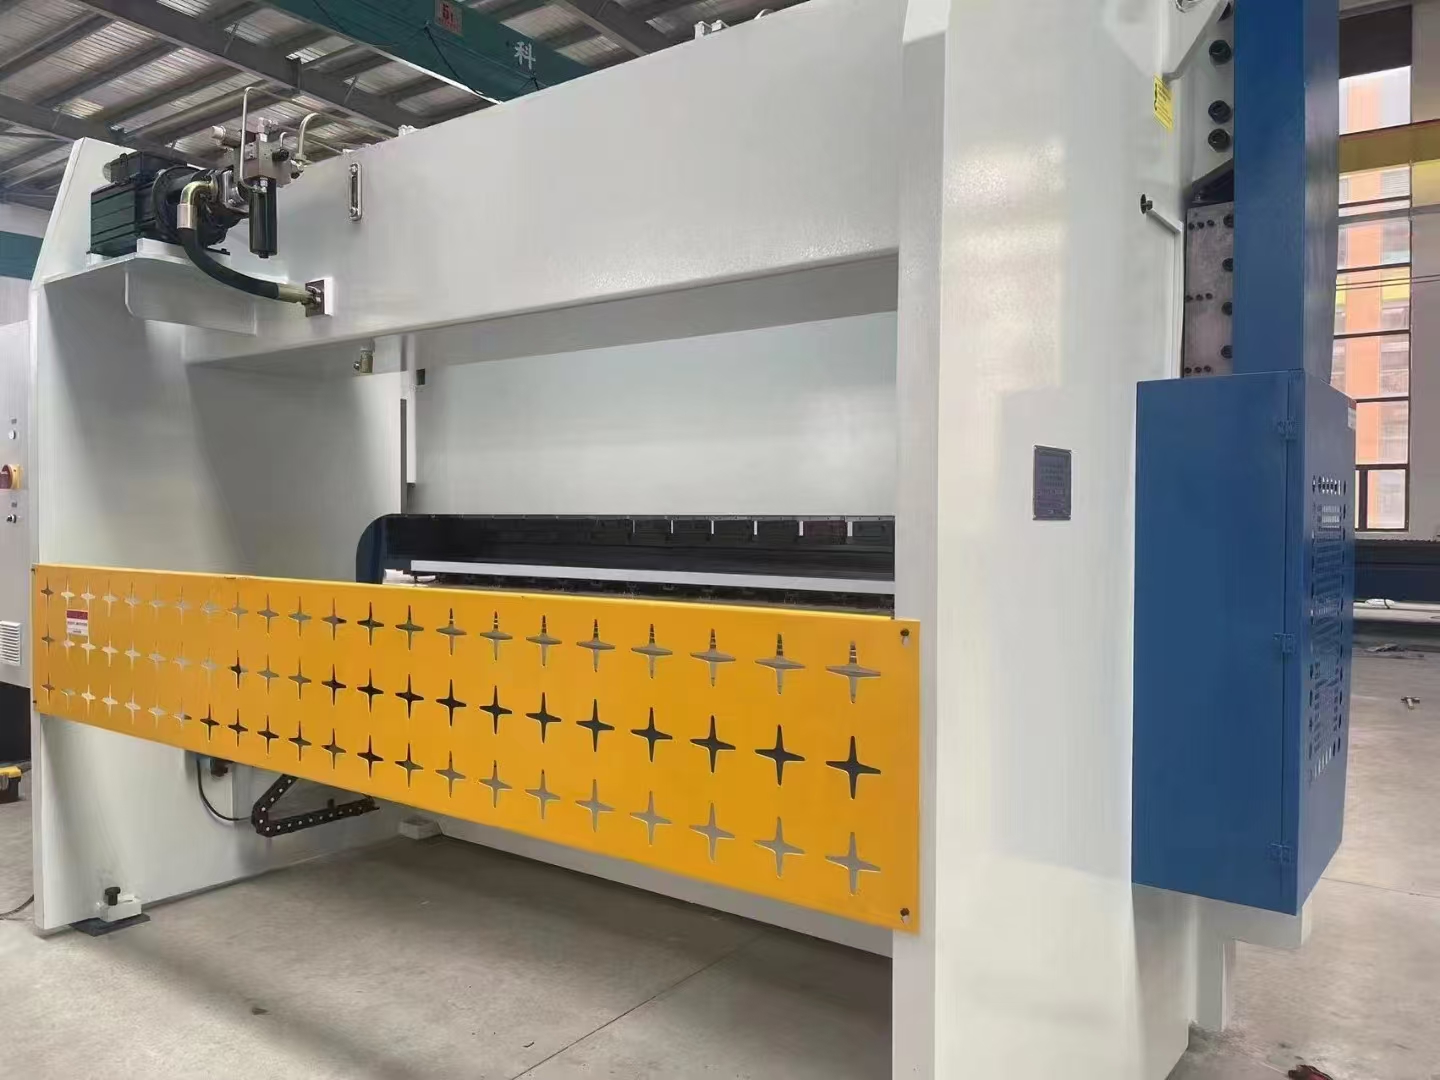
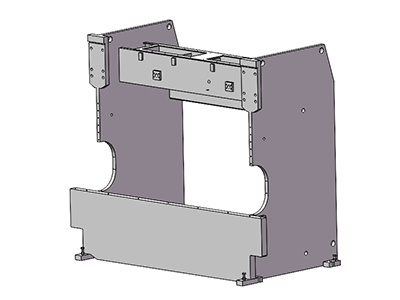
Machine tool structure 1. The CNC machine tool adopts the latest technology design, the whole steel plate welding structure, high strength, high stiffness; 2. The frame adopts German technology and uses annealing furnace as a whole to eliminate internal stress, with good precision; 3. The main component structure is analyzed and optimized by using American ANSYS/UGS/CAD/CAM/IMAN 3D software. The structural parts are cleaned by sand blasting and sprayed with anti-rust paint. 4. The column, upper working slider and lower table of the machine tool are processed by the Czech Skoda or Qiqihar II-Machine f5-axis boring and milling machine in one time to ensure the parallelism, perpendicularity and parallelism of each mounting surface. |
| Y1 ~ Y2 axis
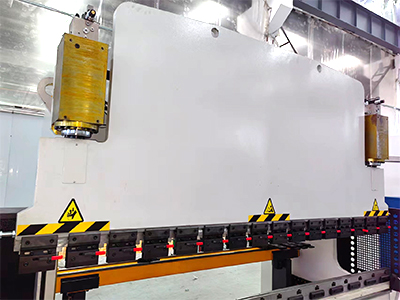
Y1 ~ Y2 axes are two independent moving axes of cylinders controlled by CNC system. Two linear scales Y1 ~ Y2 are installed at both ends of the machine, which are used to determine the exact distance between the slider and the table. The linear scale is connected with the table to eliminate the influence of the column deformation on the position of the slider. When the slider is running, the position data is immediately fed back to the numerical control system, which can calculate and output the servo valve control signal S1 ~ S2, control the output flow of the two electro-hydraulic servo valves, and synchronize the two cylinders. |
 |
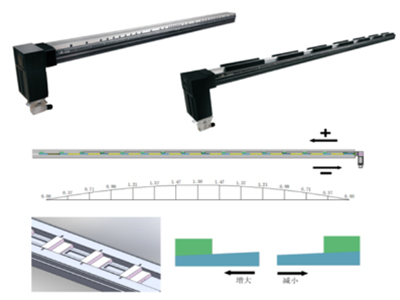 |
Anti-Deflection Table The V-axis is a CNC axis that controls the amount of convexity added to the table, allowing accurate deflection compensation over the full length of the table. The crowning table is composed of a number of integral convex wedge iron with beveled surface, which can move relative to each other to form a group of positions. The deflection compensation of the table is automatically carried out by the computer, and the accuracy of the machine is retained after several years of use. The deflection curve fits the deformation curve in the full length range so that the full length Angle is consistent. The automatic correction and compensation capability provided by the system is convenient and reliable. |
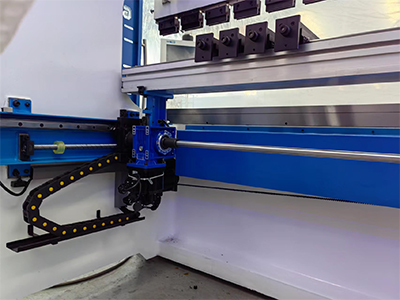
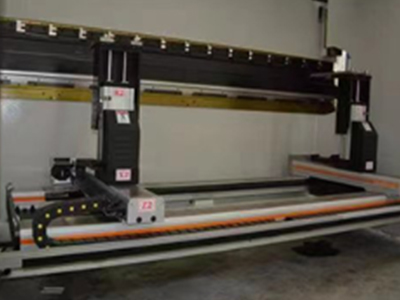
| Backgauge Controlled by servo motor, the use of large lead high-precision ball screw, with fast speed, high positioning accuracy, multi-stage gear design, increase the positioning range, so that the workpiece bending dimensional accuracy to achieve the ideal state. The beam is made of aviation cast aluminum, strong plasticity, impact resistance than iron and steel beams have more advantages. The accuracy of use is not affected by the age (the frequent use of iron and steel beams will be affected by their own weight, resulting in sinking bending deformation, so that the straightness error of the beam will grow into a geometric shape) |
 |
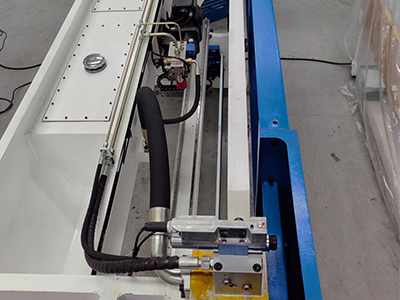 |
Hydraulic system
1. The whole system is equipped with main servo motor, saving energy and reducing noise |
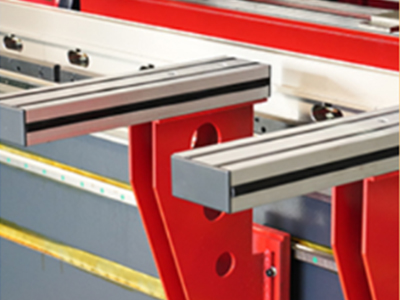 Can move in different directions |
 |
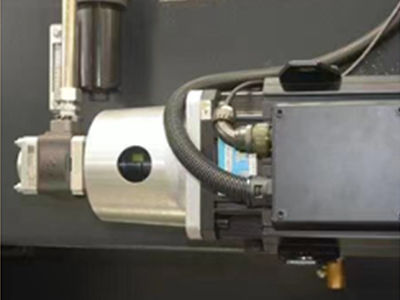 INOVANCE servo main motor |
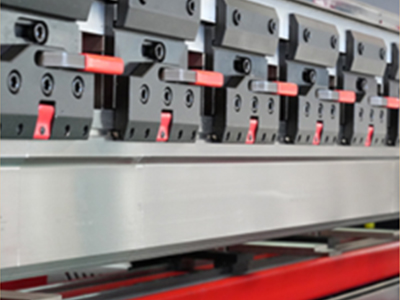 Very accurate clamping, positioning and alignment |
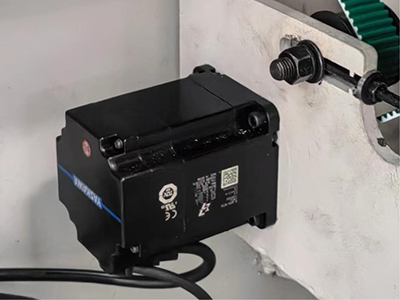 YASKAWA rear feed servo motor and drive |
 EATON clamp adapter |
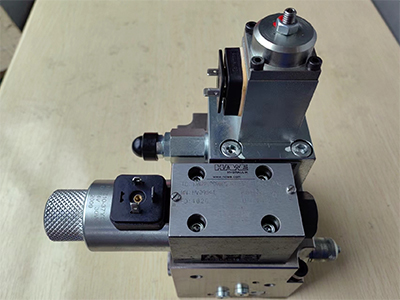 HAWE/Rexroth hydraulic valve |
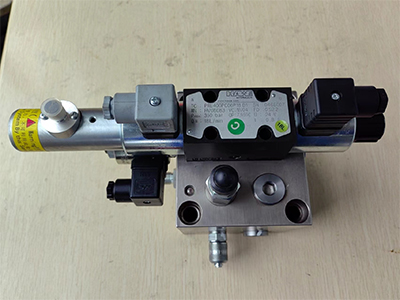 HAWE/Rexroth proportional valve |